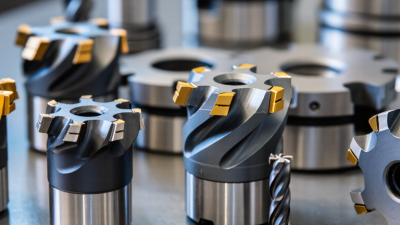
What Are Tungsten Carbide Inserts Used For?
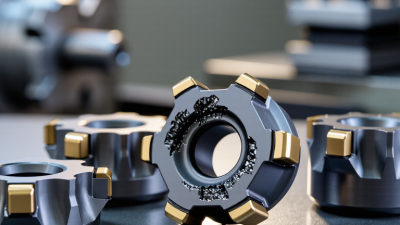
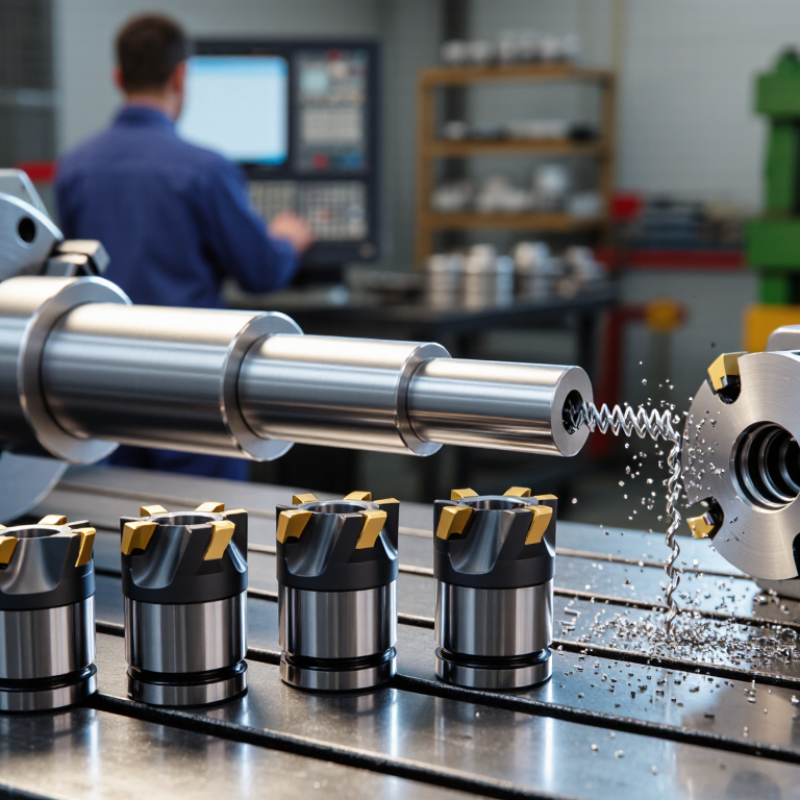
Tungsten Carbide Inserts are essential cutting tools in modern machining. They are used to shape steel, cast iron, stainless steel, aluminum, wood, and composite materials. Their hard carbide body withstands high pressure, friction, and heat during turning, milling, drilling, and boring operations. In a busy workshop, one insert may remove material from a rotating shaft while producing thousands of consistent cuts.
Their practical value comes from a careful balance between hardness and toughness. A sharp cutting edge can improve surface finish, reduce machining time, and support repeatable production. Coated grades may also resist crater wear and built-up edges during demanding applications. However, Tungsten Carbide Inserts are not universal solutions. An insert designed for hardened steel may perform poorly on aluminum. That detail is easy to overlook.
Experienced machinists usually consider material grade, cutting speed, feed rate, depth of cut, and machine stability together. Coolant selection can matter too. Dry cutting may work in some operations, while controlled coolant improves edge life elsewhere. Small changes can produce large results.
The wrong insert can chip quickly.
This article explains common uses, insert types, and practical selection factors. It also examines real workshop conditions, including vibration, interrupted cuts, and changing workpiece hardness. Some recommendations remain conditional. Tool performance depends on the entire cutting system, not the insert alone. Reliable results come from manufacturer data, measured trials, and careful observation at the machine.
Tungsten Carbide Composition: 70–97% WC with 3–30% Cobalt Binder
What Are Tungsten Carbide Inserts Used For?
Tungsten carbide inserts cut steel, cast iron, stainless steel, aluminum, and difficult alloys. They are common in turning, milling, drilling, and grooving operations. Their hardness supports high cutting speeds and longer tool life than many conventional tool materials. The USGS Mineral Commodity Summaries 2024 estimated global tungsten mine production at about 81,000 metric tons in 2023. This supply supports cutting tools, wear parts, and other industrial applications.
Tungsten carbide grades usually contain 70–97% tungsten carbide and 3–30% cobalt binder. WC provides hardness and wear resistance. Cobalt adds toughness by holding the carbide grains together. More cobalt generally improves impact resistance, while lower cobalt content can increase hardness. The balance matters. A very hard insert may chip under interrupted cutting. A tougher grade may wear faster during continuous machining. ITIA technical publications identify cemented carbide as one of tungsten’s major industrial uses. Still, composition alone does not predict performance. Grain size, edge geometry, coating, speed, feed, and coolant also matter.
Tips: Match cobalt content to the cutting load. Use tougher grades for interrupted cuts and unstable setups. Choose harder grades for steady, abrasive machining. Check the supplier’s technical data, then test one insert under real shop conditions. Small adjustments can prevent a bright edge from becoming a broken one.
What Are Tungsten Carbide Inserts Used For?
Tungsten carbide inserts are used for cutting, turning, milling, drilling, mining, and wear-resistant applications. Their composition commonly ranges from 70–97% tungsten carbide (WC) with 3–30% cobalt binder. WC provides hardness and wear resistance, while cobalt improves toughness.
The chart shows the stated composition range by mass. Higher WC content generally supports greater hardness and wear resistance, while higher cobalt content generally improves impact resistance and toughness.
Hardness and Wear Resistance: Approximately 1,600–2,200 HV
What Are Tungsten Carbide Inserts Used For?
Tungsten carbide inserts are used for turning, milling, and drilling tough materials. Their hardness typically measures about 1,600–2,200 HV, depending on grade and binder content. This extreme hardness helps resist abrasive wear from steel, cast iron, stainless steel, and nonferrous alloys. It also supports stable cutting edges during repeated production cycles.
Hardness alone does not explain their performance. Wear resistance depends on cutting speed, feed rate, coolant, and workpiece condition. A carbide insert can machine a steel shaft for many passes, while a poorly adjusted setup may damage its edge within seconds. Flank wear often appears as a narrow shiny band behind the cutting edge. Crater wear can develop across the rake face under high heat.
Small details matter. A rigid toolholder reduces vibration and protects the insert corner. Correct edge geometry also controls heat and cutting pressure. In practical use, operators should inspect the edge regularly rather than wait for visible failure. That approach saves material and avoids rough surfaces.
The 1,600–2,200 HV range is useful, but it is not a guarantee. Higher hardness may improve abrasion resistance while reducing toughness. Interrupted cuts can then cause chipping. I have found that choosing the hardest insert is not always the best decision. Material behavior, machine rigidity, and cutting conditions must be evaluated together.>
Mining and Drilling Applications Using 14.5–15.2 g/cm³ Carbide Grades
Tungsten carbide inserts are essential in mining and drilling, where rock quickly damages ordinary cutting materials. Grades with densities from 14.5 to 15.2 g/cm³ offer a practical balance between hardness, toughness, and wear resistance. They are commonly pressed into buttons, cutters, and wear pads for rotary, percussive, and down-the-hole drilling tools.
In hard rock, the insert transfers repeated impact into a small contact area. A well-selected grade can maintain a sharp working edge while resisting fracture. Higher density often indicates a greater proportion of carbide in the structure, but density alone cannot determine performance. Binder content, grain size, porosity, and heat treatment also matter. Field engineers should match these factors with rock hardness, impact energy, drilling speed, and water conditions.
Small details matter. Inspect worn inserts after each shift. Look for edge chipping, polishing, cracking, or uneven wear. These marks can reveal excessive impact, poor alignment, or an unsuitable grade. A common mistake is choosing the hardest insert for every formation. That decision may improve abrasion resistance, yet it can reduce toughness in fractured ground. I have found that drilling records are often incomplete, which makes grade selection less certain. Recording penetration rate, rotation speed, bit pressure, and failure patterns creates better evidence for future tool changes. The best choice is not always the densest grade.
ISO Insert Geometries, Coatings, and Typical Cutting-Speed Ranges
What Are Tungsten Carbide Inserts Used For?
ISO Insert Geometries, Coatings, and Typical Cutting-Speed Ranges
Tungsten carbide inserts shape, turn, mill, and thread steel, stainless steel, cast iron, and aluminum. ISO 1832:2017 classifies inserts by shape, clearance angle, tolerance, and chip-breaker style.
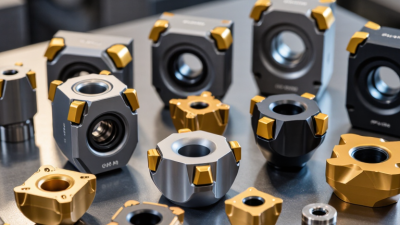
C geometry uses an 80-degree diamond, while D and V geometries offer 55- and 35-degree points. W inserts provide three cutting corners. Geometry sets the direction.
Coatings change how the insert handles heat, friction, and abrasion. CVD coatings, often based on titanium compounds and aluminum oxide, suit stable turning in steel and cast iron. PVD coatings usually support sharper edges and interrupted cuts.
Reference cutting tables in the Machining Data Handbook, 3rd edition, commonly place carbide speeds near:
120–250 m/min
for carbon steel
80–180 m/min
for stainless steel
150–300 m/min
for cast iron
300 to 1,000 m/min
Aluminum may run with a suitable polished edge.
These ranges are useful, but not absolute. ISO 3685 tool-life testing shows that speed, feed, depth of cut, and edge preparation interact strongly.
A practical starting point is often 180 m/min for medium steel, with moderate feed and coolant control. Then inspect flank wear, chips, and surface finish after several passes.
Coating is not armor. A hard interrupted cut can still fracture the edge quickly. I would not trust a catalog value without checking machine rigidity, workholding, and actual material hardness.